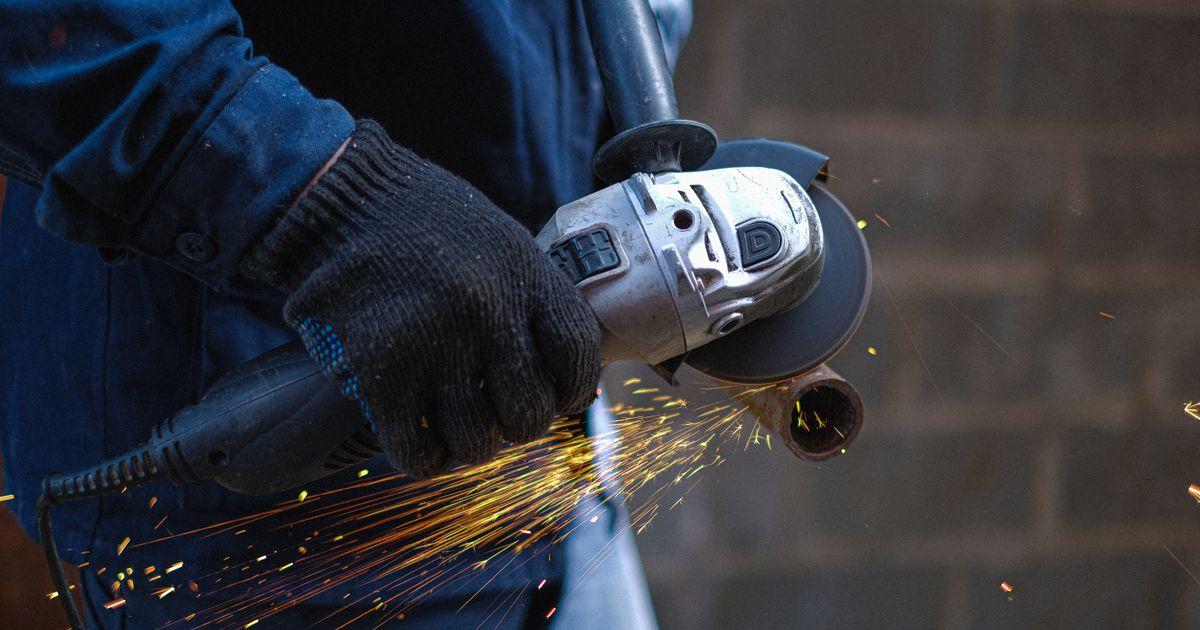
The angle grinder is the most borrowed tool on any UK site, and one of the few that can hurt you before the first cut's done. Abrasive wheel safety starts at the disc, not at the cut. Most of us were taught by a mate who was taught by someone else, and nobody checked. This one's for whoever changes the wheel, not the safety manager.
Quick answer
The short version
Safe abrasive wheel work comes down to three things: the right wheel for the machine and the job, mounted properly on clean flanges with blotters where needed, and run within the wheel's marked maximum speed. Anyone who mounts or changes wheels needs adequate training under PUWER 1998, and the guard stays on for every cut.
Summary
At a glance
- Who it is for
- Tradespeople and small contractors who use grinders and disc cutters on UK sites.
- Best next step
- Compare the speed marked on your wheels with the spindle speed marked on your machines before the next cut.
In short
Key takeaways
- The number on the wheel is its maximum permissible speed, and the machine must never run faster.
- The guard stays on for every cut. The 180 degree claim is a mangled guard requirement, not a permission.
- There's no statutory abrasive wheels certificate, but training for anyone who mounts or changes wheels is a legal duty under PUWER 1998.
Why Abrasive Wheels Hurt People on Construction Sites
A bonded wheel is hard grit held by resin or vitrified bond, spinning at tens of metres per second at its edge: up to 80 m/s on a typical grinder disc and 100 m/s on large reinforced cutting-off wheels. When one fails it doesn't slow down and stop: it bursts, and fragments leave with real energy behind them. Overspeeding matters most. Run a wheel past its marked maximum and the forces holding it together lose the argument.
The other ways are less dramatic but more common. Kickback, when the disc grabs and throws the machine back at you. Contact with the spinning edge, usually the top half people forget is turning. And fragments or sparks ejected at whoever's standing in the line of fire.
HSG17, HSE's abrasive wheels guidance, opens with a blunt stat: nearly half of all accidents involving abrasive wheels come down to an unsafe system of work or operator error. Not exotic faults. How the job was set up and how the tool was used.
Important safety warning
Never run a wheel above the maximum speed marked on it, and never fit a wheel rated lower than the machine's spindle speed. Overspeeding is one of the main causes of wheel breakage, and a bursting wheel is the most serious failure mode there is. If the markings are worn off, the wheel doesn't go on.
The Main Wheel Types and What Each One Is For
Cutting Discs vs Grinding Discs
Flat cutting discs cut a slot with the edge; depressed-centre grinding discs present the face safely for grinding. They're not interchangeable: edge-grinding with a cutting disc loads it sideways in a way it was never designed for, and face-grinding with one is a classic cause of breakage. An oversize wheel on a smaller grinder usually means taking the guard off to make room, and that's the failure chain in one sentence. Wrong wheel, guard off, overload, burst.
Diamond Blades vs Bonded Abrasive Discs
Diamond blades and bonded discs fail differently, and they're marked differently. A bonded disc wears away as it cuts; a diamond blade can seize or shed segments. Bonded discs are marked to EN 12413, diamond blades to EN 13236, and each carries its own speed rating. If a blade carries an EN 13236 mark and an expiry date, respect both.
Reading the Markings on the Wheel
What the Speed Number Actually Means
The big number on a wheel isn't the speed you set the grinder to. It's the wheel's maximum permissible speed, marked in rpm and metres per second on wheels larger than 80mm (HSG17 paragraph 13), with colour-coded stripes at 50 m/s and above. The rule that matters on the tools: the machine's spindle speed must not exceed the wheel's marked maximum.
Definition
Maximum operating speed
Wheels also carry restriction of use codes, marked per BS EN 12413 and BS ISO 525; HSG17 paragraph 14 lists RE1 to RE4 and RE6, with no RE5. Two worth knowing: RE2 means not permitted for hand-held cutting-off machines, and RE6 isn't permitted for face grinding.
Other Markings Worth Checking
Beyond speed, HSG17 paragraph 12 requires wheel marking to conform to Annex A of BS EN 12413, and Figure 1 shows what that includes: the ISO type, dimensions, specification mark, a traceable code number and mounting instructions. The traceable code matters most: it ties the wheel to its manufacture date.
Organic bonded wheels for hand-held use carry a use-by date, three years from manufacture, under HSG17 paragraph 15. The bond degrades with age and storage, so an out-of-date disc isn't a bargain, it's a spare frisbee. Check the date before the wheel goes near a spindle.
Mounting a Wheel: The Three Checks Before It Spins
Mounting is where most avoidable mistakes happen, so treat it as a process, not a five-second nut run. Three checks, in order.
Step by step
- 1Check the wheelRight type and size for the machine and the job, undamaged, and within its use-by date if it carries one.
- 2Check the speedThe wheel's marked maximum must be at or above the machine's spindle speed. No match, no fit.
- 3Mount it correctlyClean flanges, blotters where required, correct flange sizes, spindle nut snug rather than hammered down, then run it up in a safe area before cutting.
Blotters and Flanges
A blotter is the compressible liner, usually cardboard, between wheel and flanges: 0.2mm to 1.0mm thick, slightly larger than the flanges, free from wrinkles (HSG17 paragraph 55). It spreads the flange clamping force evenly, which also prevents slip and flange wear. Some wheels take no blotter: mounted wheels and points, inserted-nut discs, plate-mounted wheels, cylinder wheels in chucks, rubber-bonded cutting-off wheels 0.5mm or thinner, taper-sided wheels and threaded-insert wheels (paragraphs 55 and 56).
The general rule at HSG17 paragraph 46 is flanges at least one third of the wheel diameter, with six named exceptions for specialist wheel types. Paragraph 48 allows smaller flanges where it matters on site: reinforced resin-bonded depressed-centre grinding, depressed-centre and flat cutting-off wheels up to 230mm on portable machines, and reinforced flat cutting-off wheels on fixed and portable petrol-engined machines, where one quarter of the diameter is acceptable. Flanges should be recessed, machined true, mild steel rather than grey cast iron, and the same diameter. Don't over-tighten the spindle nut: the clamping holds the wheel, it doesn't crush it.
The Ring Test and When It Applies
Before a bonded wheel is mounted, HSG17 paragraph 18 describes the ring test: tap the wheel with a light non-metallic implement and listen. A clear ring suggests an intact wheel, a dead sound means reject. It only works on dry, sawdust-free wheels; organic bonded wheels never ring as clearly as vitrified ones; a wheel that rings can still be damaged.
Myth vs fact
Myth
Fact
Guards: What the Law Requires and the '180 Degree' Myth
The guard stays on. Full stop. PUWER 1998 regulation 11(1) requires effective measures to prevent access to dangerous parts of machinery, and the spinning wheel is the dangerous part. Regulation 11(2) puts fixed guards first in the hierarchy, so far as practicable. On portable machines the guard always sits between the operator and the wheel, and HSG17 paragraph 109 caps the gap between the guard's inside face and an unused wheel's periphery at 6mm.
Now the myth, because you'll hear it in the hut. The claim: you can remove the guard for cuts where "less than 180 degrees of the wheel is exposed", or for cuts "deeper than 5mm". Neither figure is a permission. Both numbers are real; they mean the opposite of what the myth says.
In US OSHA and ANSI material, 180 degrees is a maximum exposure angle, a limit on how much wheel the guard may leave showing. In HSG17 it's the opposite: a minimum enclosure of 175 degrees on portable machines, 180 to 270 degrees on various fixed ones. The only 5mm in HSG17 is a front lip dimension on guards for wheels over 130mm. Guard design rules got inverted into a licence to take the guard off.
Say it plainly: no UK regulation or HSE guidance permits removing or reducing the guard for a cut, and HSG17 warns that serious and often fatal accidents happen when guards are removed to fit an oversize wheel.
Myth vs fact
Myth
Fact
Kickback and Body Positioning
With the guard between you and the wheel, the last failure mode is the disc grabbing. Clamp the workpiece so it can't pinch the disc as the cut opens up, and stand so a kickback throws the machine away from you. Know where the sparks are going, keep the top half of the wheel clear of cables and ledges, and keep bystanders out of the line of fire.
Pre-Use Checks Before Every Job
Once the wheel's mounted, the rest is habit: run the same short list before the first cut of every job, not just the first job of the week.
Checklist
- Machine body, lead or battery in good condition, no exposed conductors or cracked casing.
- Guard fitted, undamaged, and positioned between you and the wheel.
- Wheel type, size and speed rating match the machine and the task.
- Wheel visually sound, clean and dry, and within its use-by date if marked.
- Eye protection suitable for grinding, plus the rest of the PPE the task needs.
- Workpiece secured so it cannot pinch the disc mid-cut.
- Bystanders clear and the spark path pointed somewhere safe.
PPE and Dust: The Bits People Skip
Grinding PPE gets treated as optional the moment the job runs late. HSG17 paragraph 158 says eye protectors should be worn in all dry grinding operations, or transparent screens fitted to fixed machines, so impact-rated eye protection is the floor. Add gloves, boots and hearing protection, and check the fit, not just the presence.
Two hazards deserve their own guides. Cutting concrete or stone creates silica dust, a COSHH substance with its own control regime: see silica dust from cutting concrete and stone. Prolonged grinding also passes vibration into your hands; our hand-arm vibration from prolonged grinding guide explains where that leads.
A grinder blows past the noise action levels quickly, so check our guide to noise limits and hearing protection before you decide the earmuffs live in the van.
PUWER: Training, Mounting and Inspections Today
Who Can Change or Mount a Wheel
Start with the correction, because trade content still gets this wrong: the Abrasive Wheels Regulations 1970 are gone. PUWER 1998 revoked the whole instrument via regulation 39 and Schedule 4, in force 5 December 1998. Any course or blog post citing the 1970 Regulations as current law is out of date, and the old "appointed person" scheme died with them.
PUWER regulation 9 is the training duty: adequate training for all who use work equipment, extending to those who supervise or manage its use. Regulation 7 restricts use of equipment posing a specific risk to the people given the task of using it, and restricts repairs, modifications, maintenance and servicing to people specifically designated for it, who must themselves be trained. Mounting isn't named in regulation 7, but HSG17 is equally blunt: it's only for an appropriately trained person.
There's no such thing as a statutory "abrasive wheels certificate". HSG17 says training courses usually provide a certificate of attendance, not competence, and HSE names statutory certificates only for things like chainsaws, lift trucks and drivers. The legal duty is adequate training, not a document. If an inspector comes asking, it's your training arrangements they look at; our guide to what an HSE inspector looks for on site covers how that goes.
Inspection Frequency and Who Can Inspect
PUWER regulation 6 is the inspection duty, and grinders qualify: equipment exposed to deterioration liable to cause dangerous situations is inspected at suitable intervals, and each time exceptional circumstances occur that could jeopardise its safety. Results are recorded under regulation 6(3), and kept until the next inspection.
HSG17 paragraph 123 recommends for portable electric grinders: 240-volt machines get a daily user safety check, a weekly formal visual inspection by a competent person, and a combined inspection and test before first use, then every month. For 110-volt machines, it's a weekly safety check, a formal visual inspection, and a combined inspection and test every three months. Pre-use checks don't normally need recording; formal inspections do.
Who counts? HSE is refreshingly unbureaucratic: anyone with sufficient knowledge and experience to know what to look at, what to look for, and what to do if they find a problem. No external certification needed.
Source-backed note
HSE note
The Abrasive Wheels Regulations 1970 were revoked in whole by the Provision and Use of Work Equipment Regulations 1998, via regulation 39 and Schedule 4, in force 5 December 1998. PUWER regulation 9 requires adequate training for all persons who use work equipment and for those who supervise or manage its use. HSG17 states that nearly half of all accidents involving abrasive wheels are due to an unsafe system of work or operator error.
Putting It Into Your Risk Assessment and RAMS
All of this collapses into a few method statement lines: wheel types and sizes, the speed check before mounting, guard position, the PPE list, spark and bystander control. Write it once, brief it when the job changes, and it becomes the way your firm does it.
Common mistakes
- Using the wrong disc type for the task, like edge-grinding with a flat cutting disc.
- Taking the guard off 'just for this cut'.
- Skipping the speed check between the wheel marking and the machine spindle.
- Running a wheel past its use-by date or with the markings worn off.
- No control over spark path or bystanders when cutting near other trades.
- Grabbing whatever grinder is nearest instead of the one rated for the wheel and the job.
Next step
Get your RAMS sorted
Grinder work belongs in your RAMS: wheel selection, speed checks, guards, PPE and spark control written down before the job starts. RAMS Builder turns your trade and task into a clear document in minutes, a solid starting point to check against the job and the site.
Related reading
Compliance note
General guidance, not legal advice
This article is general guidance, not legal advice. It reflects the position as at November 2026. Treat it as a solid starting point and give it a proper check against the job, the site and your own training arrangements before you rely on it.